

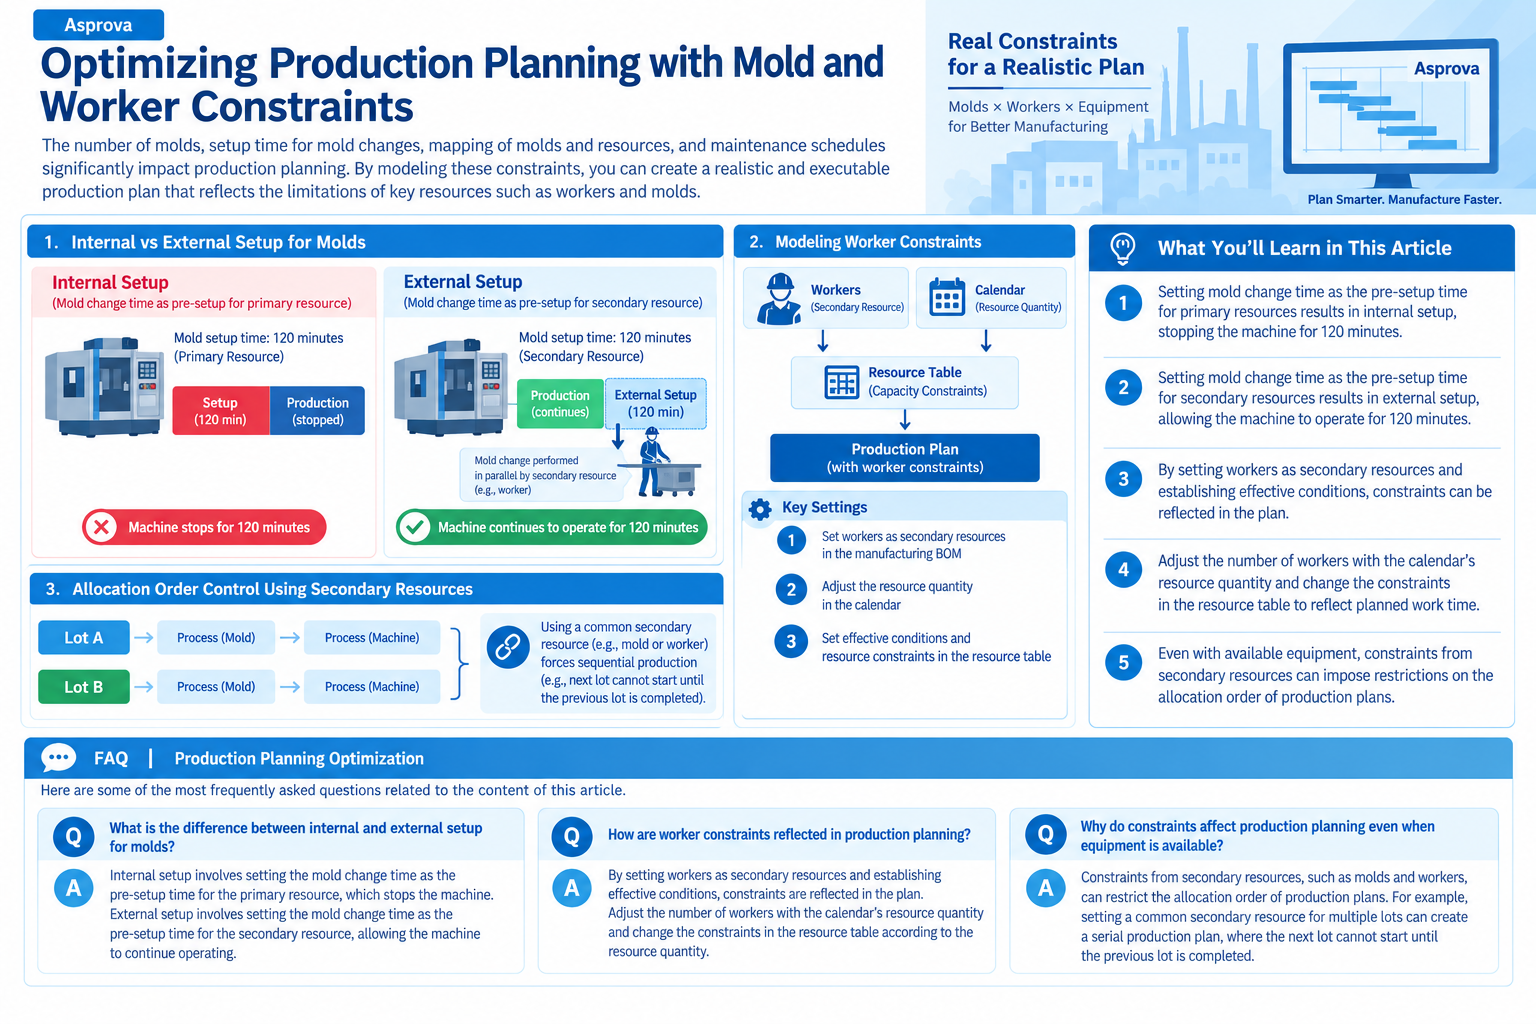
In Japanese factories in Indonesia, planning is not determined solely by the rated capacity of machines. The number of molds owned, mold changes (setup), and operator skills simultaneously affect the situation, often leading to scenarios where work cannot commence even if equipment is available.
Positioning of this article: This is the authoritative source on "sub-resource constraints (mold and operator)" under the production scheduler hub. It discusses how to place sub-resources against main resources in Asprova and how to express internal/external setup. For product overview, refer to Asprova, for weighted optimization refer to Solver, and for planning AI demo surroundings refer to Solver8.
-
-
Production Scheduler in Indonesia
Production planning and load planning are closely related and require verification based on quantities. It is important to compare production quantities,…
続きを見る
What this article covers
- This article is the authoritative source on sub-resource constraints (mold and operator) in production schedulers (APS).
- Placing mold change as a pre-setup for the main resource results in internal setup (machine stop), while placing it on the sub-resource side results in external setup (machine continues operation).
- Operators are also treated as sub-resources, and their planning workload can be reflected using resource availability conditions and calendar resource quantities.
- Even if there is available equipment, placing common sub-resources can create constraints that serialize between lots.
- In Indonesian multi-variety and setup factories, not only machine capacity but also the number of molds owned and skills tend to become bottlenecks.
- The entire product can be traced back to Asprova, optimization exploration to Solver, and planning AI surroundings to Solver8.
Why Molds and Operators are Central to APS
Production schedulers (APS) allocate orders to resources with finite capacity. In Indonesian multi-variety and setup factories, the following simultaneously become constraints:
- The number of molds owned (limited number of molds can be used simultaneously)
- Setup time for mold changes (internal or external setup)
- Compatibility between molds and equipment (which machine can use which mold)
- The number, skills, and shifts of operators
- Non-operational slots due to maintenance, etc.
Plans that ignore these will look neat on a Gantt chart but will halt on the shop floor. In Asprova, molds and operators are treated as sub-resources to influence the main resource plan.
Mold Constraints|Internal and External Setup
By setting sub-resources in the manufacturing BOM and setting the pre-setup tasks of main and sub-resources to 0 or blank, you can express only the constraint of the number of molds owned without incurring pre-setup time.
On the other hand, where to place the exchange time changes the meaning in the plan.
- Internal Setup — Set mold change time as pre-setup for the main resource. Example: 120 minutes pre-setup for main resource CUT, 0 for sub-resource pre-setup. The machine stops during the exchange.
- External Setup — Set mold change time as pre-setup for the sub-resource. Example: Blank for main resource pre-setup, 120 minutes for sub-resource pre-setup. The machine continues to operate during the exchange.
Even for the same "120-minute mold change," incorrect placement of internal/external setup can skew evaluations of load, delivery time, and setup frequency. Choosing according to actual field operations (whether molds are changed on the machine or offline) is fundamental to APS design.
Operator Constraints|Resource Availability Conditions and Resource Quantity
Operators are also treated as sub-resources like molds and can be constraints on the main resource plan. Set the resource availability conditions on the sub-resource side to establish conditions under which operators can operate.
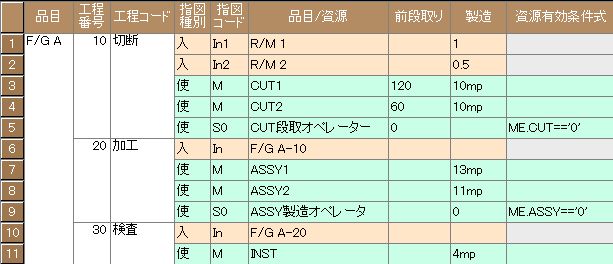
Assign operators as sub-resources to the main resources used in the process work (pre-setup or manufacturing). Adjust the number of people with the calendar's resource quantity, and reflect it in the planned work time by changing the resource table's resource quantity constraint according to the resource quantity.
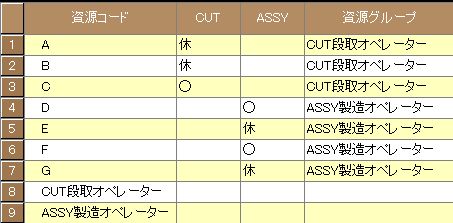
- Set sub-resources (operators) in the relevant process of the manufacturing BOM
- Set the resource constraint of operators in the resource table to infinite capacity (first visualize overload)
- Increase the calendar's resource quantity while observing the load and adjust to a feasible number of people
If the skill map (who can handle which process) is weak, increasing the number of people will not improve the plan. In Indonesian factories, sub-resources are designed in conjunction with the progress of multi-skilled workers.
Constraining Allocation Order Even with Equipment Availability
If equipment is available, the scheduler assigns work to available equipment aiming for the shortest completion. However, if there is a constraint such as "the next lot cannot start until the previous lot is finished," placing common sub-resources on both processes can create a serial (sequential) plan.
Thus, sub-resources are not only for "shortages of people or molds" but also a means of expressing order constraints. This is a standard practice when translating the field sense of "unable to start despite available machines" into planning logic.
Reading as Knowledge
- This article — Placement of sub-resources like molds and operators (constraint modeling)
- Solver — Optimization exploring conflicting objectives with weighting
- asprova-cost — Linking planned labor hours and quantities to standard costs/budgets
- Production Management Hub — ERP side for results, inventory, lots (receptacle for execution results of plans)
Frequently Asked Questions|Mold and Operator Constraints
As knowledge of production schedulers (APS), frequently recurring questions are organized.
How do you incorporate mold and operator constraints into the plan?
This article is the authoritative source. In Asprova, molds and operators are treated as sub-resources to influence the main resource plan, reflected through internal/external setup, resource availability conditions, and calendar resource quantities (URL: https://bahtera.jp/en/asprova-operator-schedule/).
What is the difference between internal and external setup?
Internal setup places the exchange time in the pre-setup of the main resource, stopping the machine. External setup places it on the sub-resource side, expressing mold change while keeping the machine running.
How are operator constraints incorporated into the plan?
Operators are made sub-resources, and their number and operability are reflected through resource availability conditions and calendar resource quantities. Skill conditions are also expressed here.
Why can't work start even when equipment is available?
It is due to a shortage of sub-resources like molds or operators, or because common sub-resources for order constraints are serializing. A view based solely on machine capacity is insufficient.
What is the difference with Solver and Solver8?
This article is about constraint modeling. Solver is for weighted exploration of objectives, and Solver8 is about planning AI demo surroundings.
Related Links
- Production Scheduler Hub — Entry point for planning, APS, and Asprova
- Asprova — Product authoritative source (Data Bridge / Viewer / Solver)
- Solver8 — Planning AI and demo surroundings
- Scheduling Optimization
- Mold and Operator Constraints
- Standard Costs and Budgets
- Solver (Optimization Exploration)
- Production Management Hub — ERP and results side